
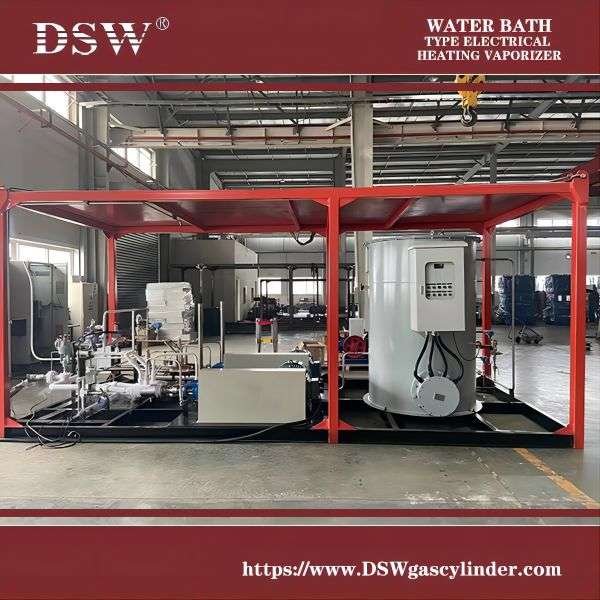
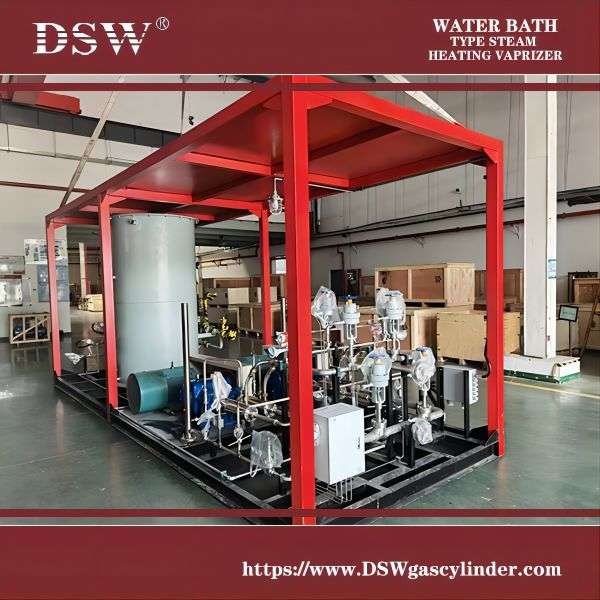
DSW Industry provides steam-heated water bath vaporizers for high-capacity gas vaporization in petrochemical plants, industrial gas facilities, and cryogenic processing installations. These systems use steam to heat a water bath, transferring heat to compatible liquefied gases through an immersed tube bundle.
With rated capacities ranging from 500 Nm³/h to 195,000 Nm³/h, the vaporizers can be configured to accommodate up to three gas streams in one unit, depending on process requirements. Their design supports controlled heat transfer, rapid load changes, and convenient maintenance for demanding industrial gas supply applications.
For other equipment configurations and vaporization technologies, explore our industrial cryogenic vaporizers.
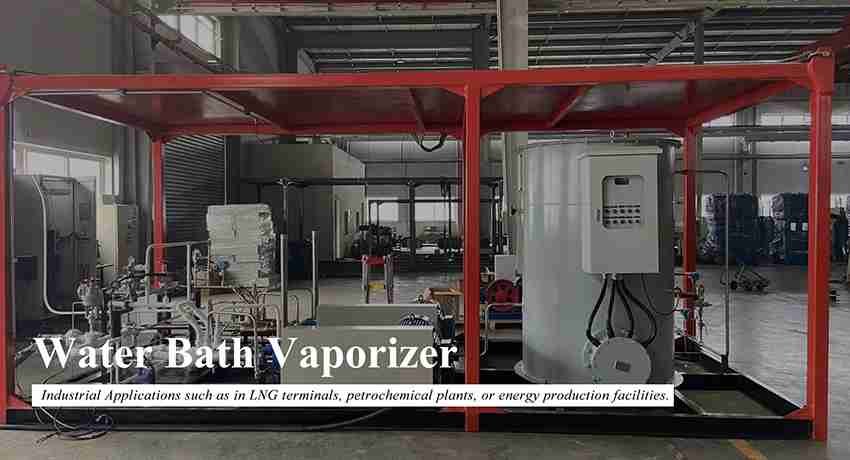
Working Principle and Design
Water Bath Heating and Temperature Control
The vaporizer consists of a water vessel containing a submerged coiled tube bundle. Steam lances heat the water bath, and heat transfers through the tube walls to the liquefied gas flowing inside the tubes. This indirect heat-transfer process vaporizes the liquid under controlled operating conditions.
Temperature controllers regulate the bath temperature to support stable operation. During standby, a miniature steam lance maintains the water temperature at approximately 60°C, helping keep the unit ready for increased demand.
Coiled Tube Bundle and Heat Transfer
The coiled tubes are connected to ring-shaped distribution and collection headers that distribute the incoming liquid and collect the vaporized gas. This arrangement supports heat transfer and accommodates changes in operating load.
The tube bundle is designed to reduce material stress during load and temperature changes. Its removable construction also provides convenient access for inspection, cleaning, and maintenance.
Startup Performance and Maintenance
Water circulation relies on buoyancy and gravity. According to the specified design performance, the vaporizer can reach full capacity within two minutes. An optional water-circulating pump system can reduce availability time to less than 10 seconds under specified operating conditions.
The removable tube bundle simplifies inspection and cleaning, helping support maintenance efficiency and equipment availability.
Key Features and Performance
High Capacity and Multi-Stream Operation
- Wide Capacity Range: Rated flow capacities from 500 Nm³/h to 195,000 Nm³/h for large-scale industrial gas requirements.
- Multi-Stream Capability: Configurations can accommodate up to three gas streams in one unit, subject to process design and fluid compatibility.
- Flexible Configuration: Equipment arrangements can be evaluated according to required capacity, process conditions, and project specifications.
Rapid Load Response and Standby Temperature
- Rapid Load Response: The specified design can reach full capacity within two minutes.
- Standby Temperature Control: A miniature steam lance maintains the water bath at approximately 60°C during standby.
- Optional Rapid Availability: Additional water-circulating pumps can reduce availability time to less than 10 seconds under specified operating conditions.
Maintenance, Noise Control, and Optional Heating
- Removable Tube Bundle: Facilitates inspection, cleaning, and maintenance.
- Noise and Erosion Control: An optimized steam injection arrangement is designed to reduce steam hammering, erosion, and noise emissions.
- Alternative Heating Options: Warm-water heating or electric heating arrangements may be available upon request, subject to project requirements.
Applications and Compatible Gases
Steam-heated water bath vaporizers are used in industrial gas processing, petrochemical facilities, and cryogenic installations where a controlled heat source is required to vaporize liquefied gases. Depending on the equipment configuration, process conditions, and material compatibility, applications may include the following.
Liquid Oxygen, Nitrogen, and Argon
- Liquid Oxygen (LOX): Oxygen supply systems for industrial processes requiring appropriately designed vaporization equipment.
- Liquid Nitrogen (LIN): Industrial nitrogen supply and process gas installations.
- Liquid Argon (LAr): Argon vaporization for industrial gas distribution and process applications.
LNG, Ethylene, and Propylene
- Liquefied Natural Gas (LNG): LNG vaporization and regasification systems for gas supply and energy facilities.
- Ethylene: Petrochemical processes requiring vaporization of liquefied ethylene.
- Propylene: Petrochemical applications requiring vaporization of liquefied propylene.
The suitable configuration depends on the process fluid, required gas flow, operating pressure, outlet temperature, materials, and applicable safety requirements. Fluid compatibility should be confirmed during engineering.
Integration with Cryogenic Storage and Gas Supply Systems
Water bath vaporizers can be integrated into industrial gas supply installations to convert stored cryogenic liquids into gas for downstream processes. Depending on the application, the system may include cryogenic storage tanks, liquid transfer piping, pressure-control equipment, instrumentation, and gas distribution lines.
For integrated equipment solutions, explore DSW Industry’s cryogenic storage solutions and industrial gas supply systems. For LNG projects, see our LNG cryogenic storage tanks.
Vaporizer Selection and Customization
Selecting a suitable steam-heated water bath vaporizer requires evaluating the process fluid, required vaporization capacity, operating pressure, inlet conditions, outlet temperature, available steam supply, and installation environment. Multi-stream requirements, control arrangements, maintenance access, and optional circulating pumps should also be considered during engineering.
To help determine a suitable configuration, provide the following project information:
- Type of liquefied gas
- Required vaporization capacity in Nm³/h
- Operating pressure and required outlet temperature
- Inlet liquid conditions
- Available steam supply conditions or preferred alternative heating source
- Number of process streams and expected load variations
- Installation environment and applicable design standards
DSW Industry can evaluate project requirements and discuss suitable vaporizer configurations for industrial gas and cryogenic applications. Contact our team with your process data to discuss equipment selection and customization.

Reviews
There are no reviews yet.